EDM
Dedicated EDM machines across the platform. The right process when conventional machining cannot hold the tolerance, the material is too hard to cut mechanically, or the feature geometry can only be produced with EDM.
EDM
Complex Geometry. Exactly as Designed.
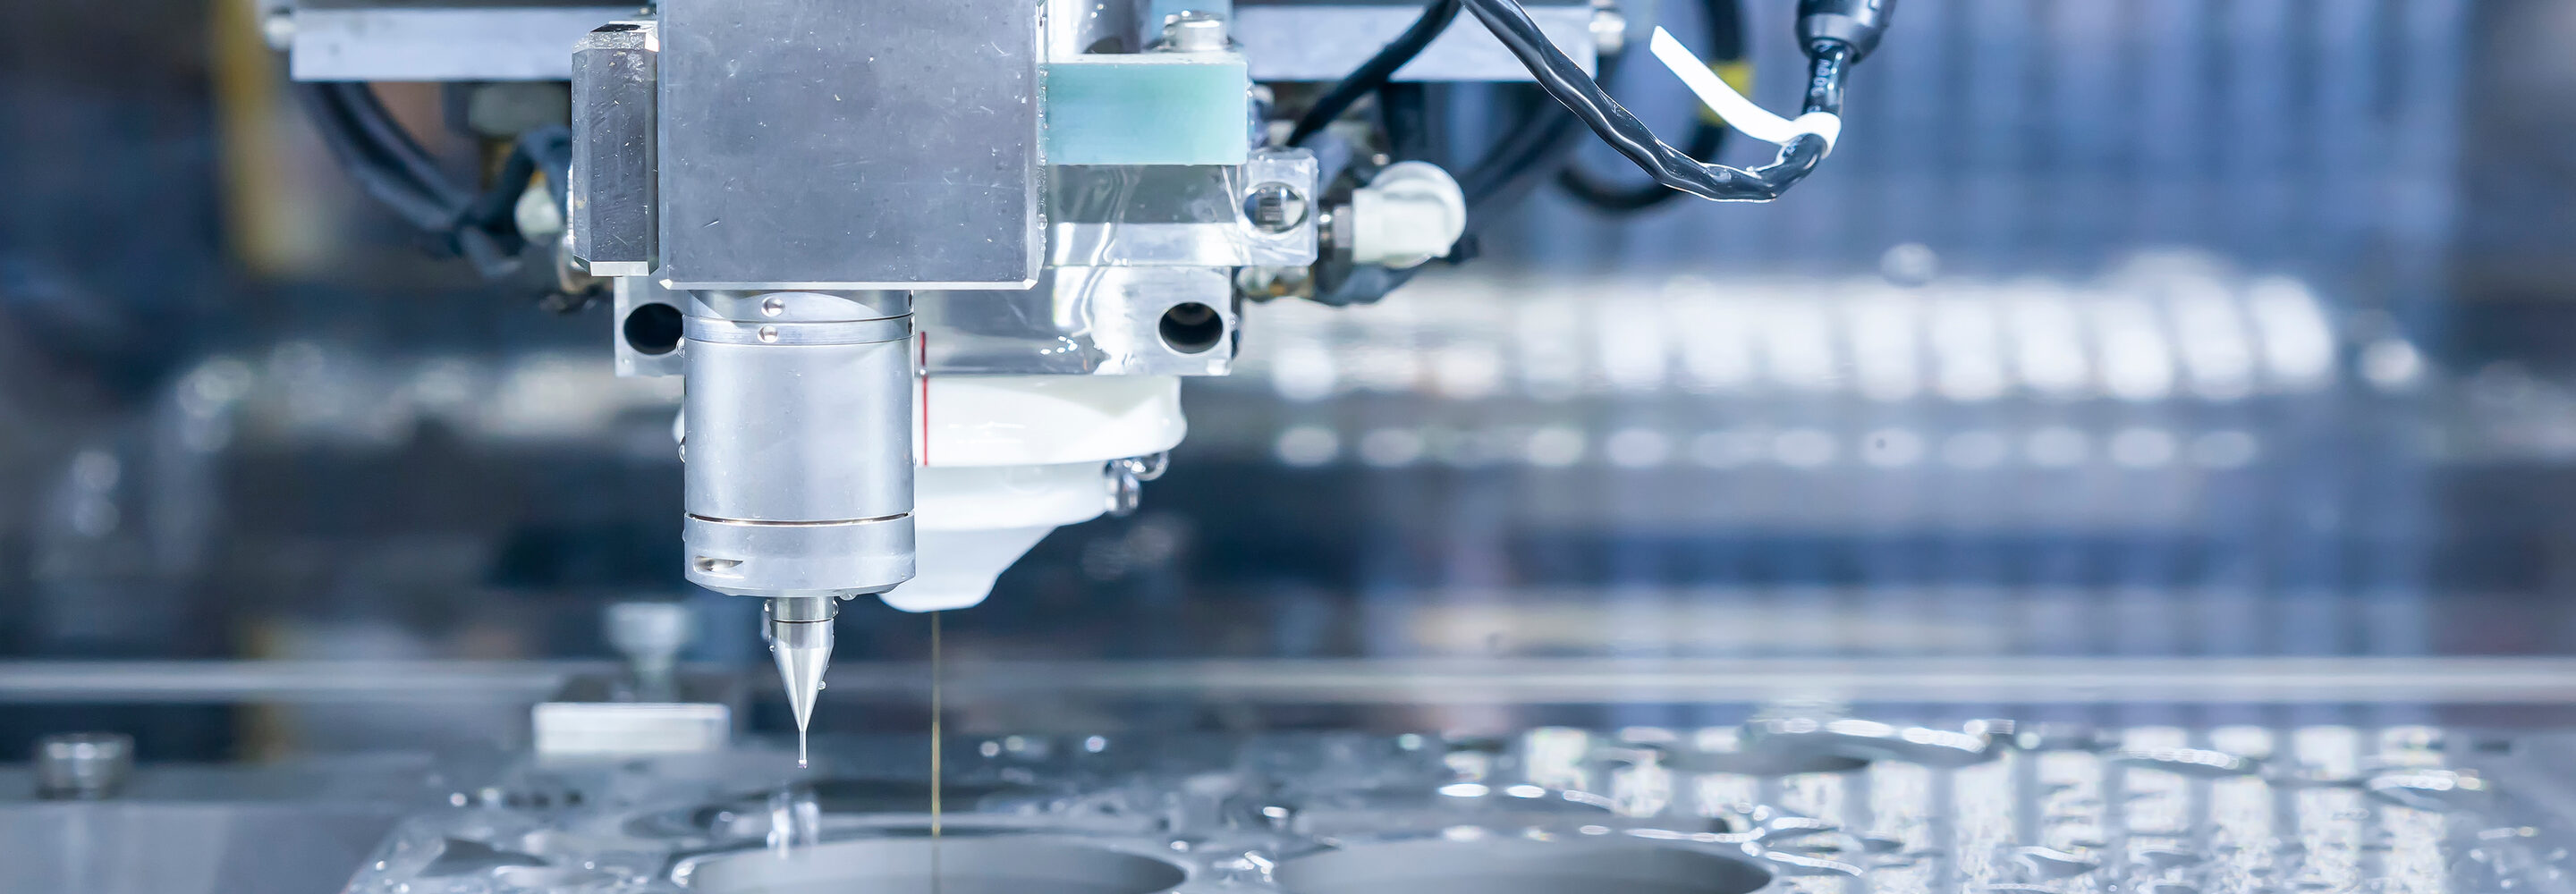
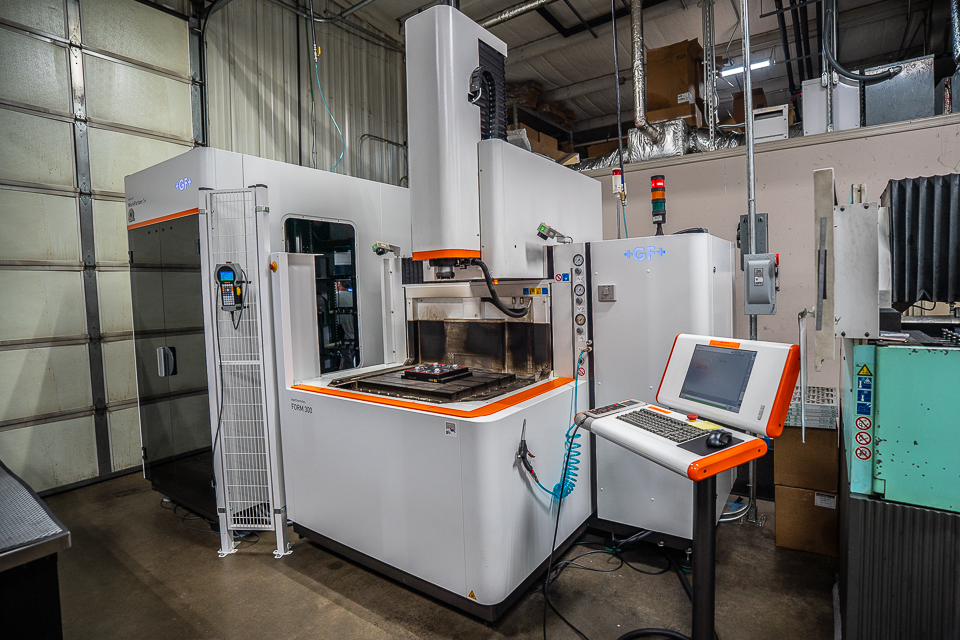
EDM removes material with controlled electrical sparks instead of a cutting tool. Wire EDM uses a thin, electrically charged wire to cut precise profiles, slots, and internal shapes through a part, while sinker EDM plunges a shaped electrode into the material to form cavities, blind pockets, and detailed 3D features. For many parts it’s the only way to produce the geometry the design calls for, including sharp internal corners, deep narrow features, and fine detail in hardened materials. And because the tool never touches the part, there’s no cutting force to deflect thin walls or push tight features out of tolerance.
The process holds tight tolerances on difficult materials, produces clean repeatable features, and works on conductive materials that would be impractical to machine otherwise. Facilities across the platform cover wire EDM, sinker EDM, and CNC hole drilling EDM.
EDM
Accu-Tool
Apex, NC
Advanced Machining & Tooling
Salisbury, NC
Douglas Machining Services
Winona, MN
Trutron Corporation
Troy, MI
EDM
Where EDM Delivers Beyond Conventional Machining
- Hardened tool steel dies, punches, and mold inserts, where a conventional cutter would deflect against the hardened material before it holds tolerance
- Aerospace and defense parts requiring tight-profile slots, keyways, and internal splines
- Semiconductor capital equipment: precision apertures, slots, and profiles in aluminum and stainless
- Medical device components with fine features or thin-wall geometries that cannot tolerate cutting force
EDM
EDM Capacity Without Bottlenecks
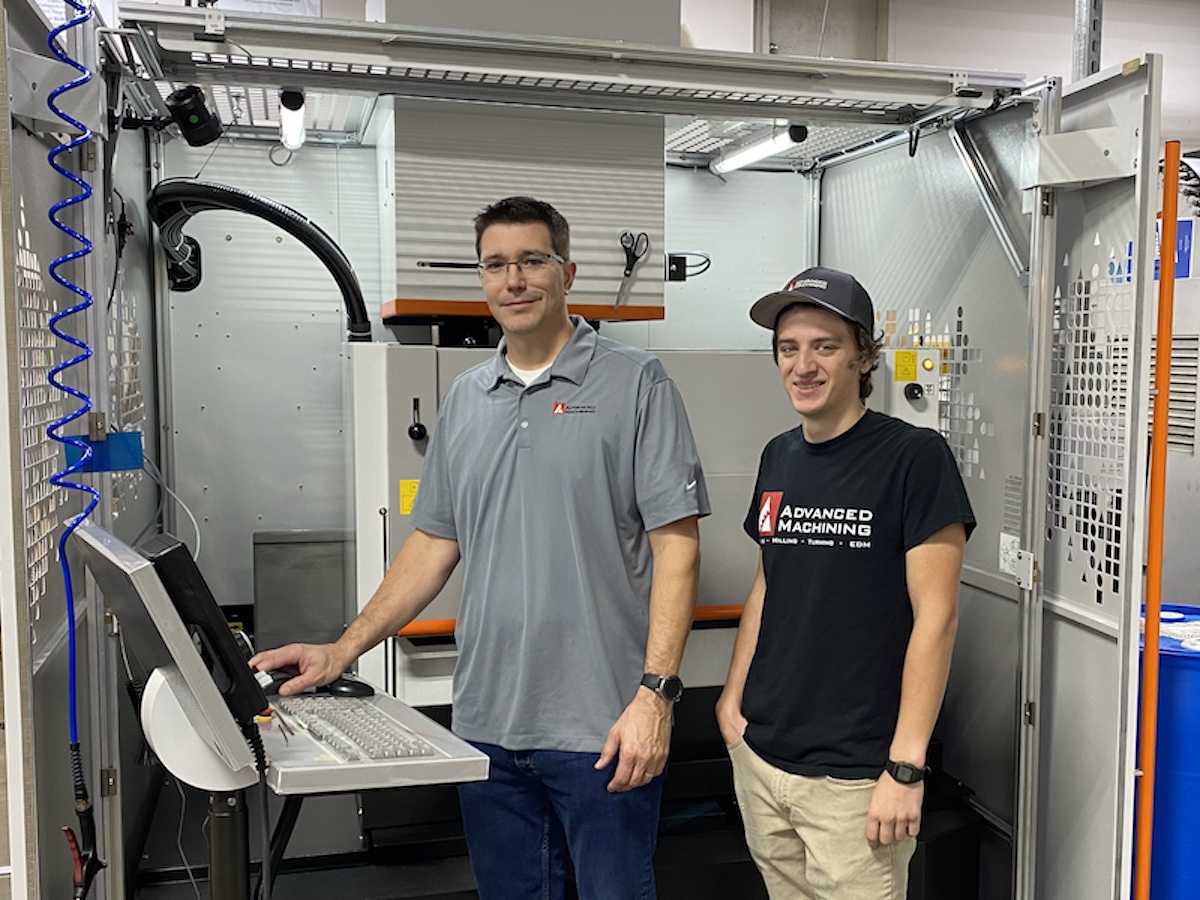
EDM is frequently the constraint in a precision shop. High setup time and limited machine availability stretch lead times. With dedicated EDM capacity across multiple facilities, Compass Precision carries EDM at a scale most single-site suppliers cannot offer. Programs that need EDM as part of a broader machining scope get it without competing with the rest of the shop’s backlog. Robotic automation lets EDM run 24/7 lights-out, so long jobs keep moving overnight and through the weekend.
| Location | Machining | Turning | EDM | Secondary | Metrology | Fabrication | Certifications | |||||||||||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 3-Axis | 4-Axis | 5-Axis | Horizontal | Automation | CNC | Mill/Turn | Swiss | Hole Popper | Sinker | Wire | Grinding | Heat Treat | Finishing | CMM | SPC | Vision | Assembly | Bending | Laser | Stamping | Welding | AS9100D | ISO 9001:2015 | CMMC | ITAR | |
| Accu-Tool Apex, NC | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | |||||||
| Advanced Machining Salisbury, NC | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ○ | ● | |||||||||||
| Bergeron Machine Westford, MA | ● | ● | ● | ● | ● | ● | ● | ○ | ● | |||||||||||||||||
| Douglas Machining Winona, MN | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ||||||||||||||
| Gray Manufacturing Denver, NC | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ○ | ● | ||||||||||||
| Pocasset Machine Bourne, MA | ● | ● | ● | ● | ● | ● | ● | ● | ||||||||||||||||||
| Quality Products Charlotte, NC | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ○ | ● | ● | ● | |||||
| R&D Machine Oldsmar, FL | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | |||||||||||
| Strom Manufacturing North Plains, OR | ● | ● | ● | ● | ● | ● | ● | ● | ● | ○ | ||||||||||||||||
| Tri-Tec Industries Charlotte, NC | ● | ● | ● | ● | ● | ● | ● | |||||||||||||||||||
| Trutron Corporation Troy, MI | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ● | ||||||||
EDM
Not Sure If EDM Is the
Right Process for Your Part?
With wire EDM, sinker EDM, and CNC hole drilling EDM across the Compass Precision platform, let’s review your geometry, material, and tolerance requirements to identify the right EDM process and facility for your program.